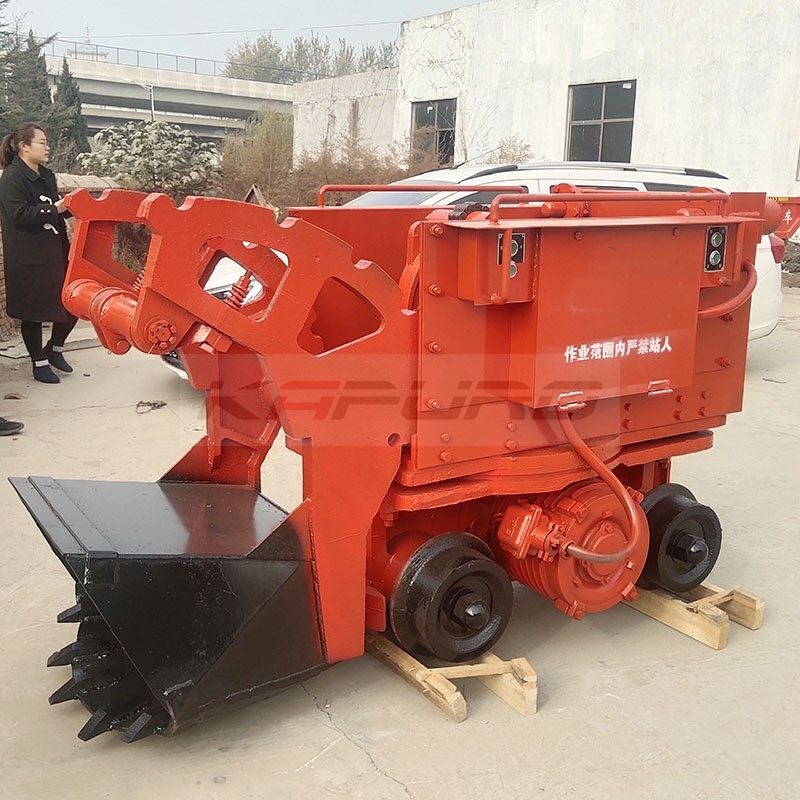
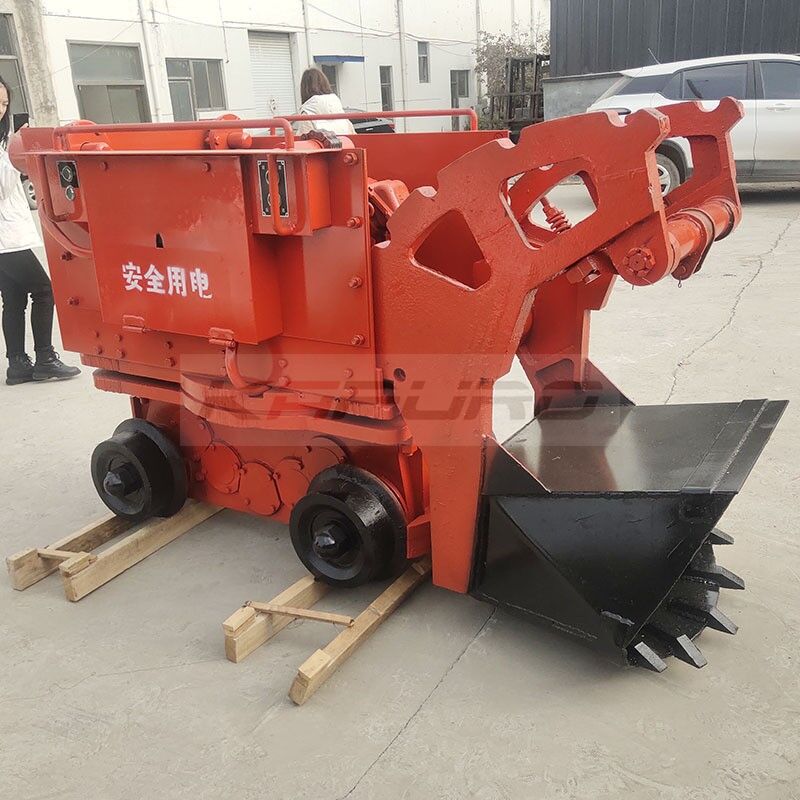
Exceptional Durability and Low Maintenance Requirements
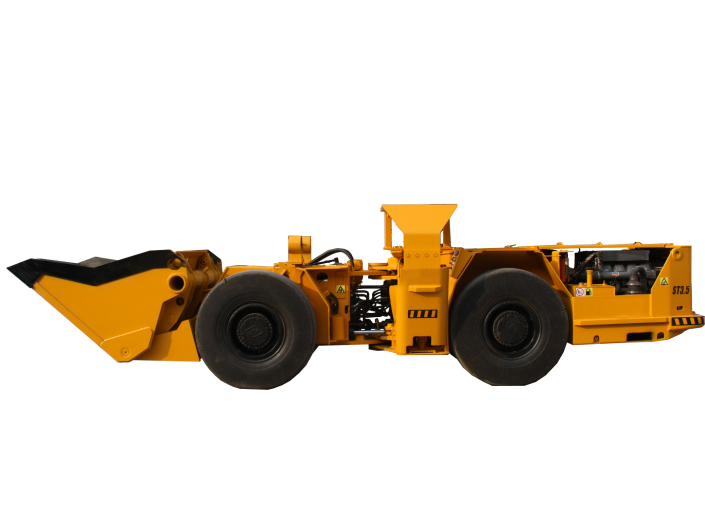
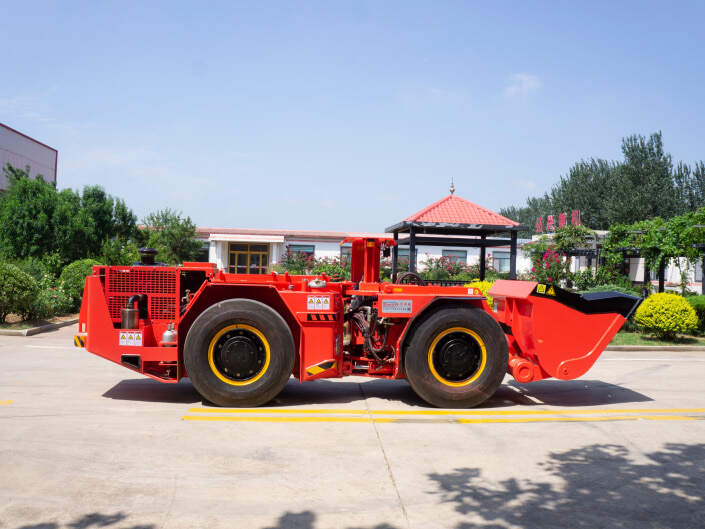
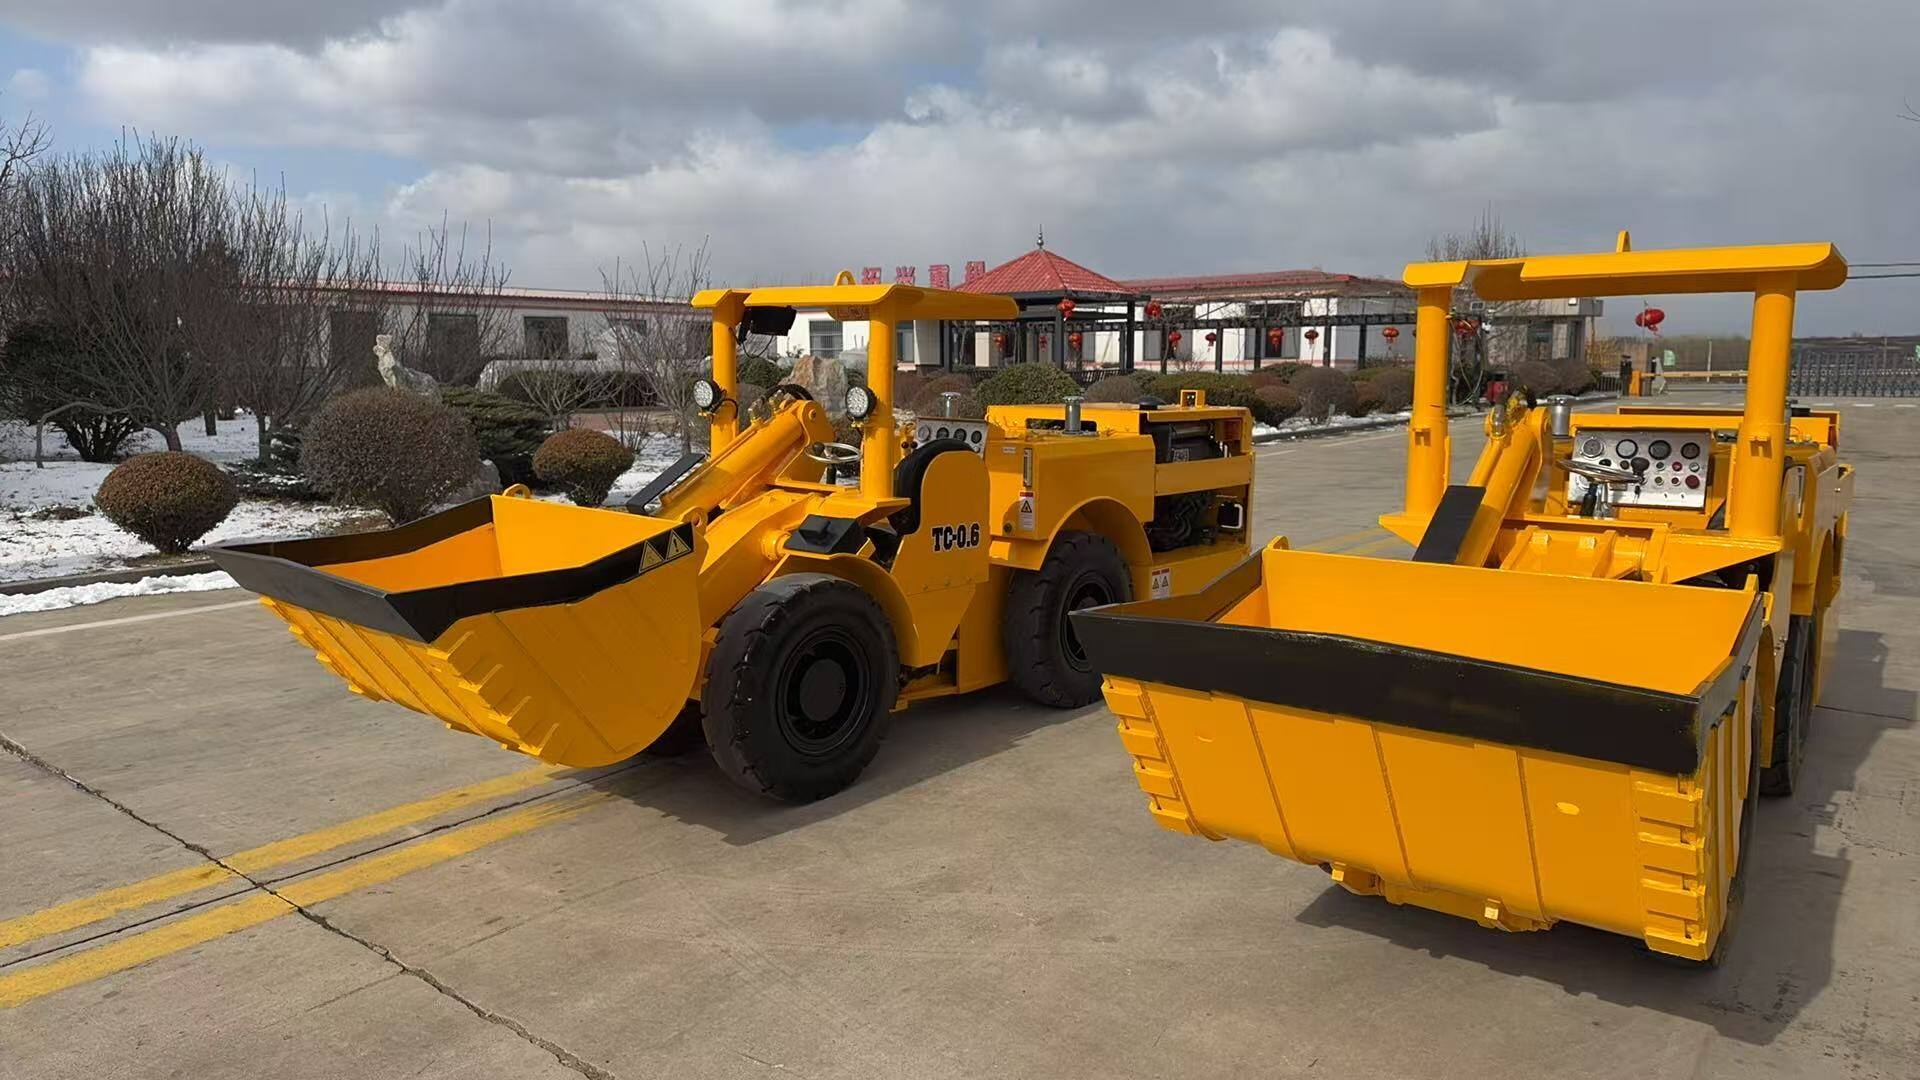
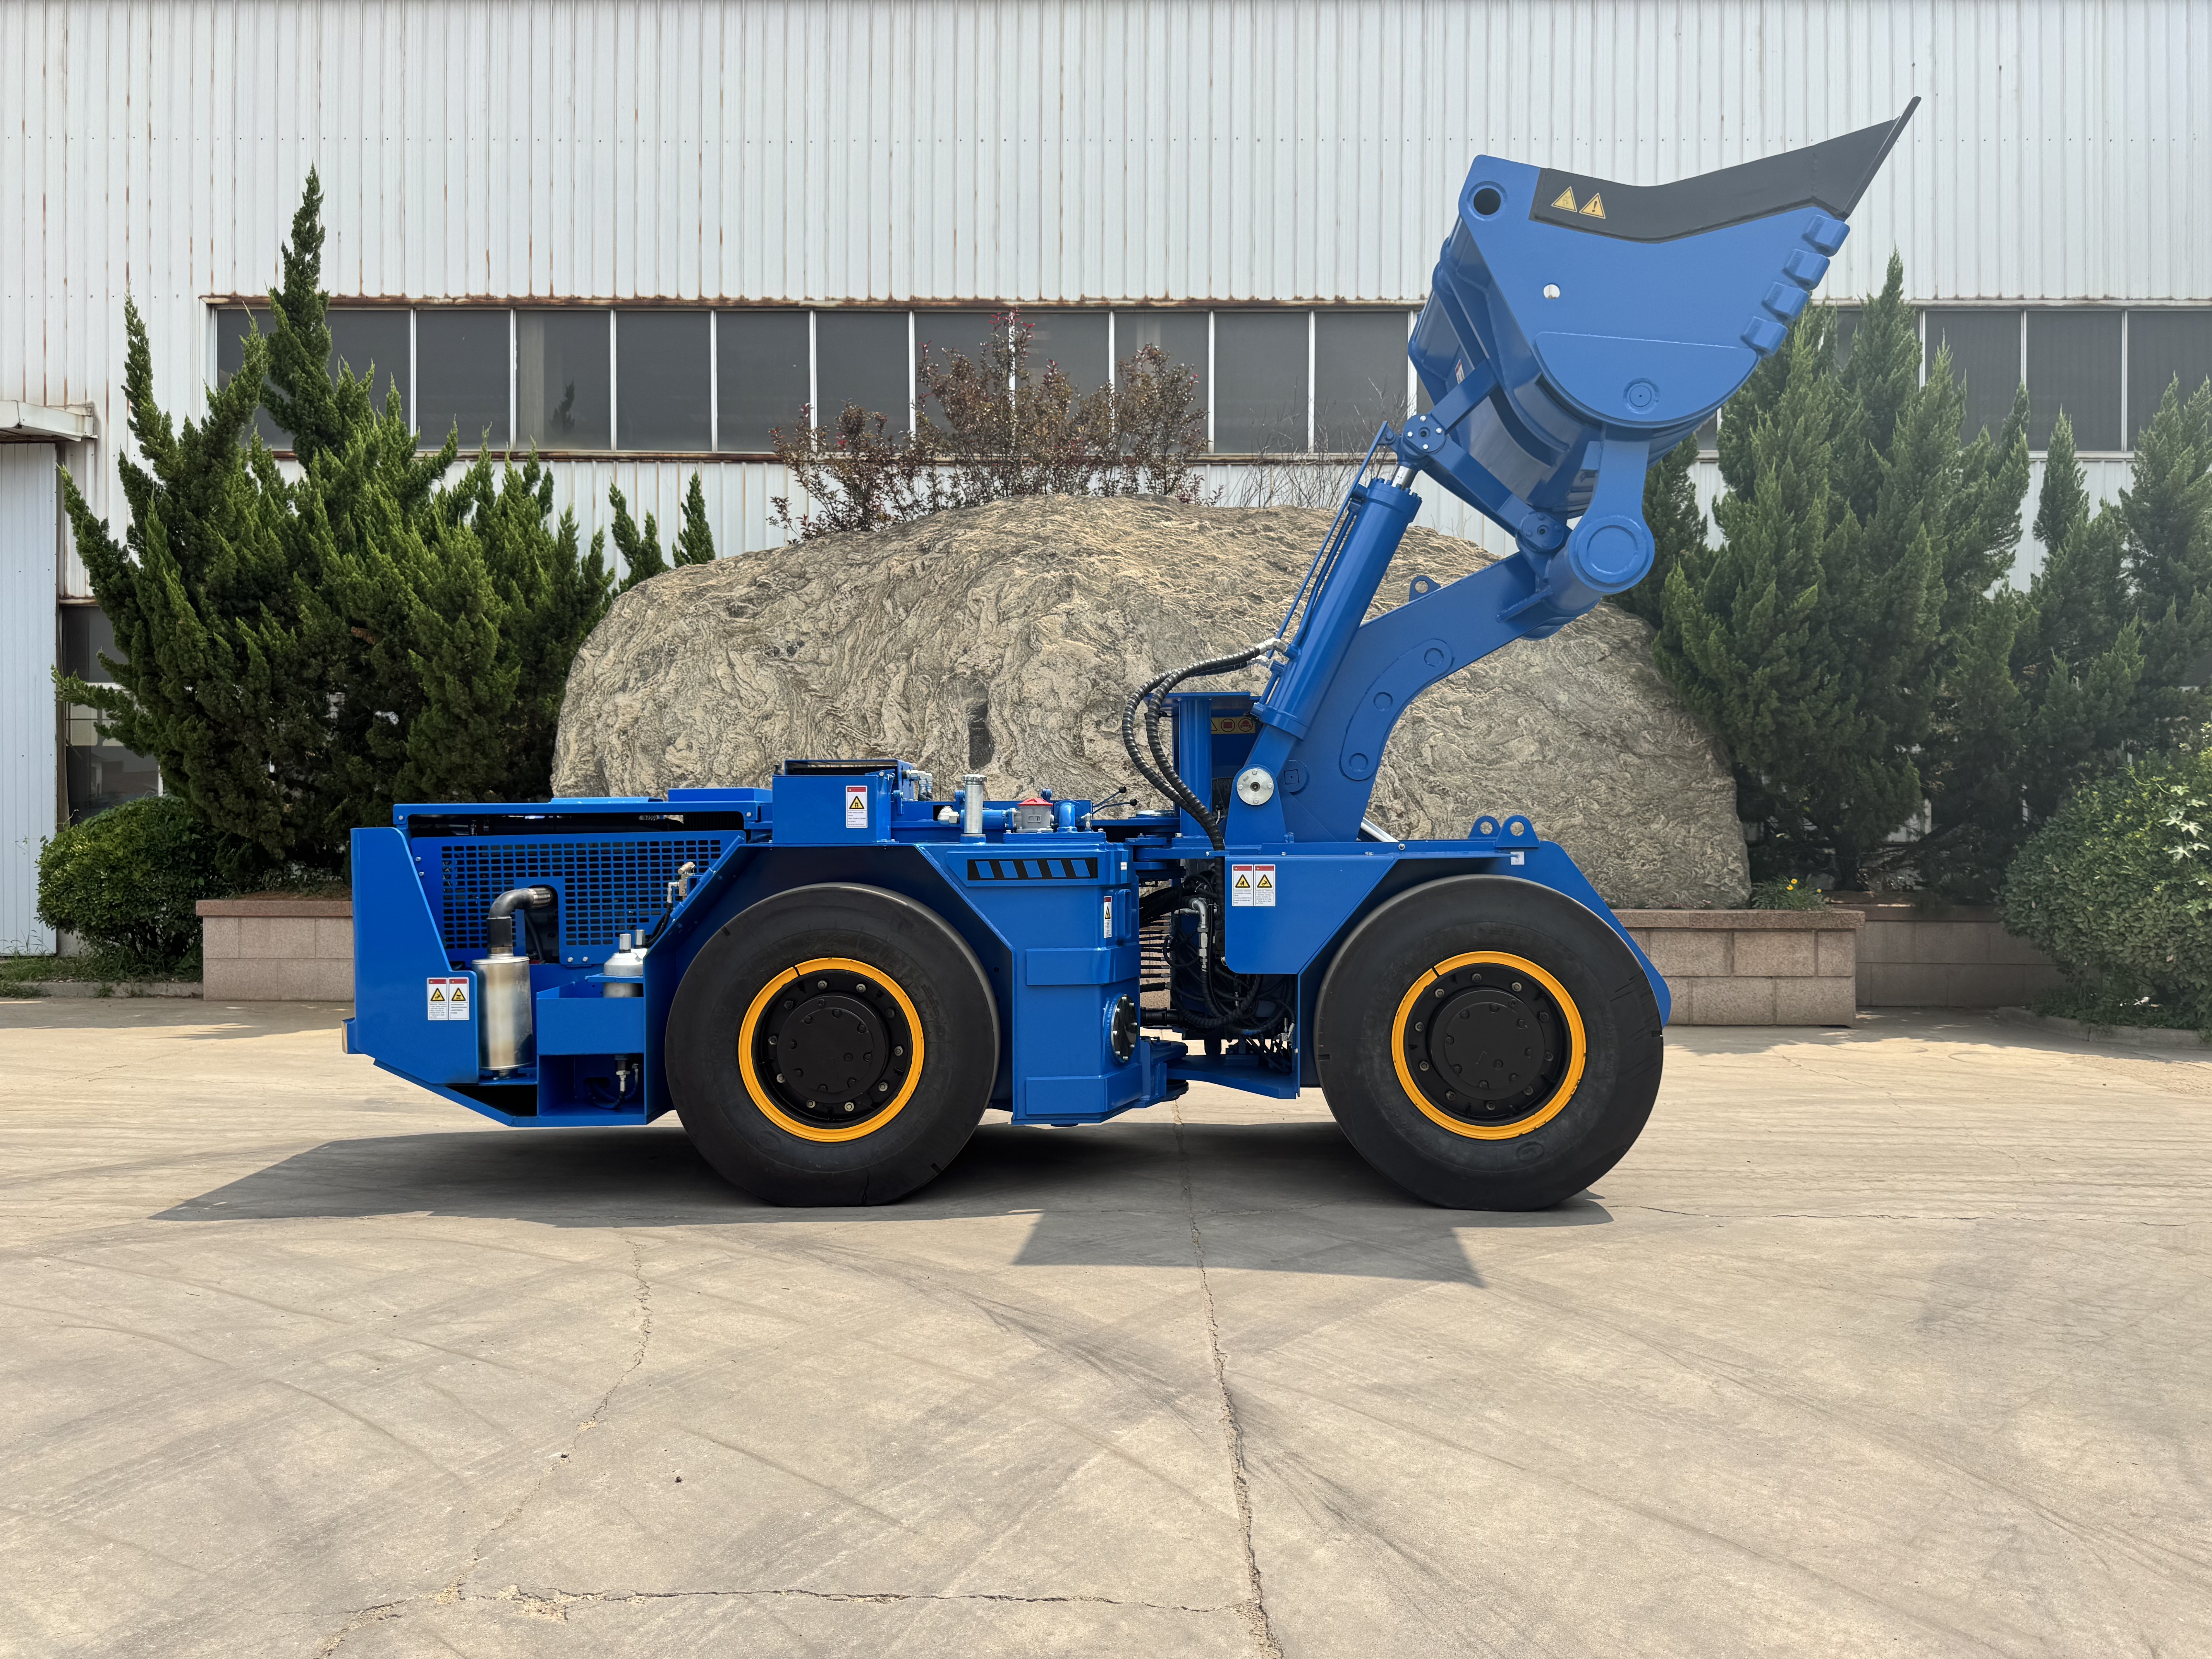
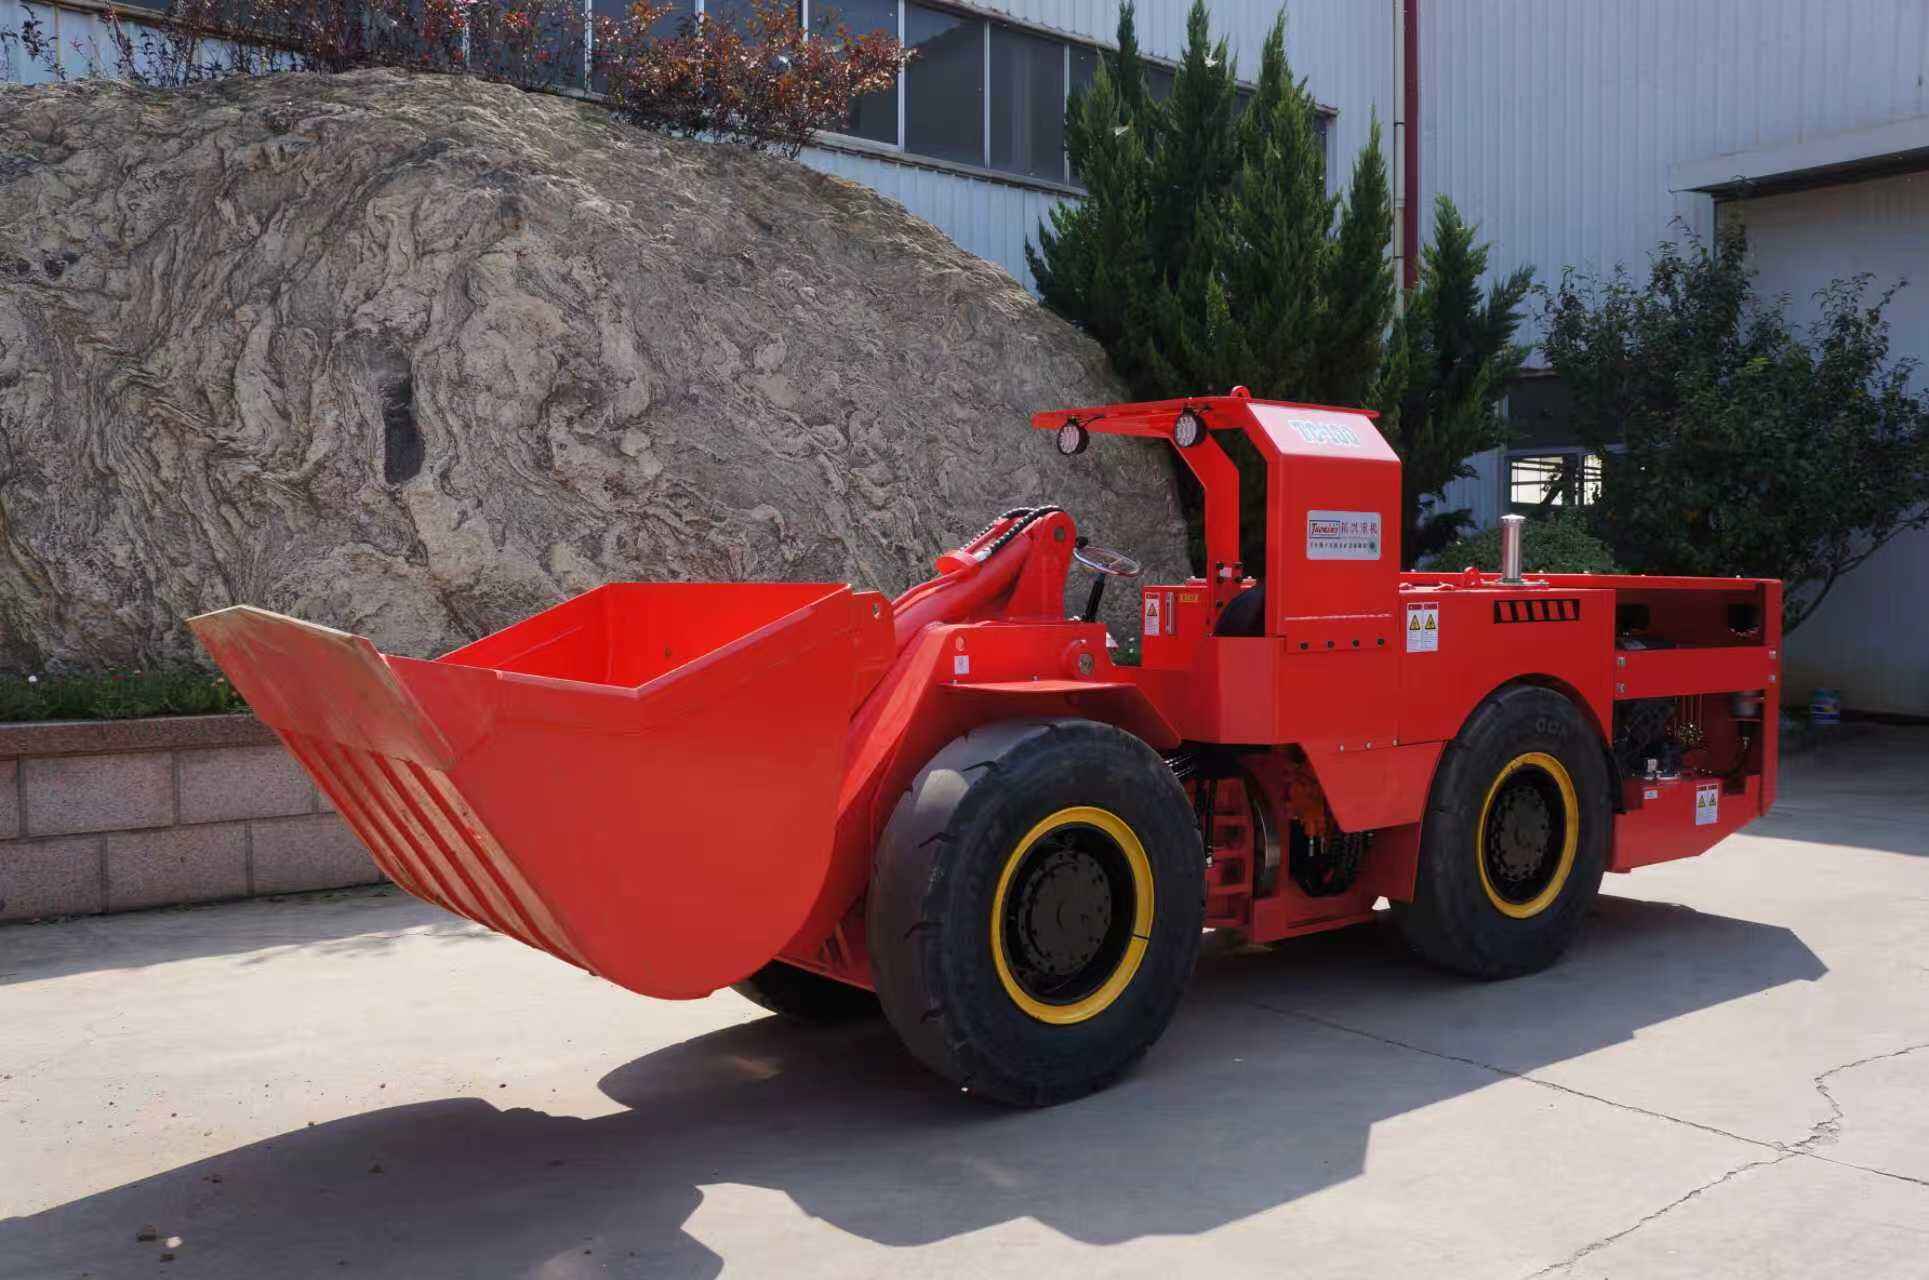
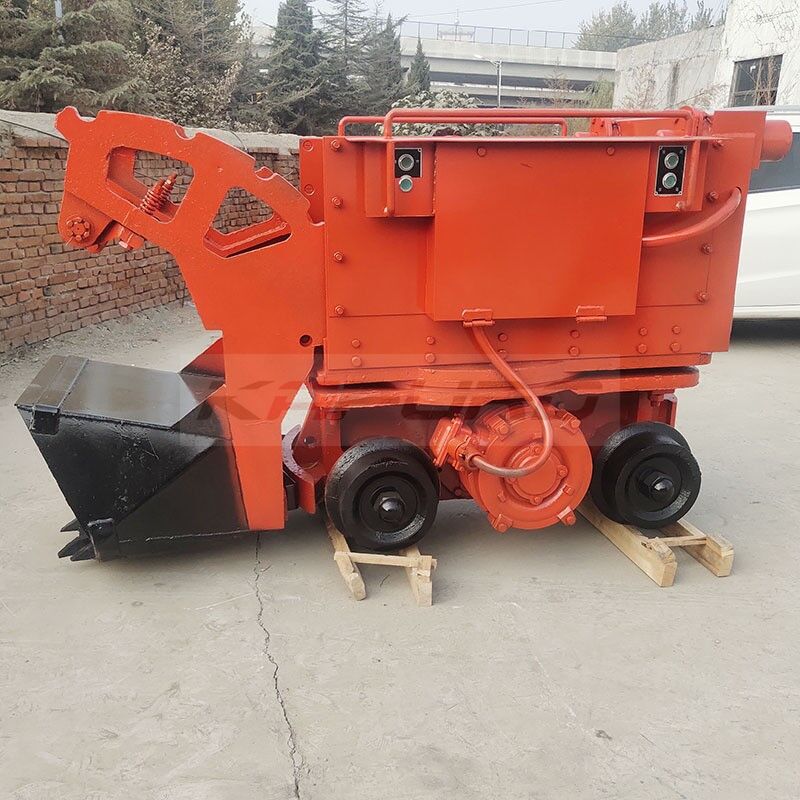
The mining rock loader is engineered specifically to withstand the punishing conditions that define mining environments, delivering exceptional durability that minimizes downtime and reduces total cost of ownership over the equipment lifecycle. Heavy-duty frame construction utilizes high-strength steel alloys selected for their superior resistance to impact, abrasion, and fatigue, ensuring structural integrity even after years of aggressive loading in rocky, abrasive materials. Critical stress points receive additional reinforcement through strategic bracing and gussets that distribute loads effectively, preventing crack initiation and propagation that could lead to catastrophic failures. The hydraulic system components are sealed and protected against contamination from dust, mud, and debris that pervade mining operations, maintaining consistent performance and preventing premature wear that degrades efficiency. Sealed pivot points and bushings eliminate the need for frequent greasing while protecting against abrasive particle intrusion, significantly reducing maintenance labor requirements and ensuring smooth operation throughout service intervals. The mining rock loader features modular component design that facilitates rapid replacement of wear items without extensive disassembly, getting equipment back into production quickly after routine maintenance or unexpected repairs. Convenient service access points are strategically located to enable maintenance technicians to check fluid levels, inspect components, and perform routine services without requiring special tools or dangerous access procedures. Extended service intervals on critical components like hydraulic oil, filters, and drive train elements reduce the frequency of planned downtime, allowing operations to maximize productive hours and minimize disruptions to production schedules. Comprehensive onboard diagnostic systems continuously monitor equipment health parameters including hydraulic pressures, fluid temperatures, and electrical system performance, alerting operators and maintenance personnel to developing issues before they cause failures. Remote monitoring capabilities available on advanced mining rock loaders enable fleet managers to track equipment performance, usage patterns, and maintenance needs across multiple machines from a central location, optimizing maintenance scheduling and resource allocation. The corrosion-resistant coatings and protective treatments applied to frame components and hydraulic cylinders extend equipment life in humid underground environments and corrosive surface conditions where untreated metals would deteriorate rapidly. Proven component suppliers and standardized parts across equipment lines ensure replacement parts availability and reduce inventory costs for operations maintaining multiple machines, simplifying procurement and reducing spare parts investment requirements while ensuring rapid repair capability when needed.
 EN