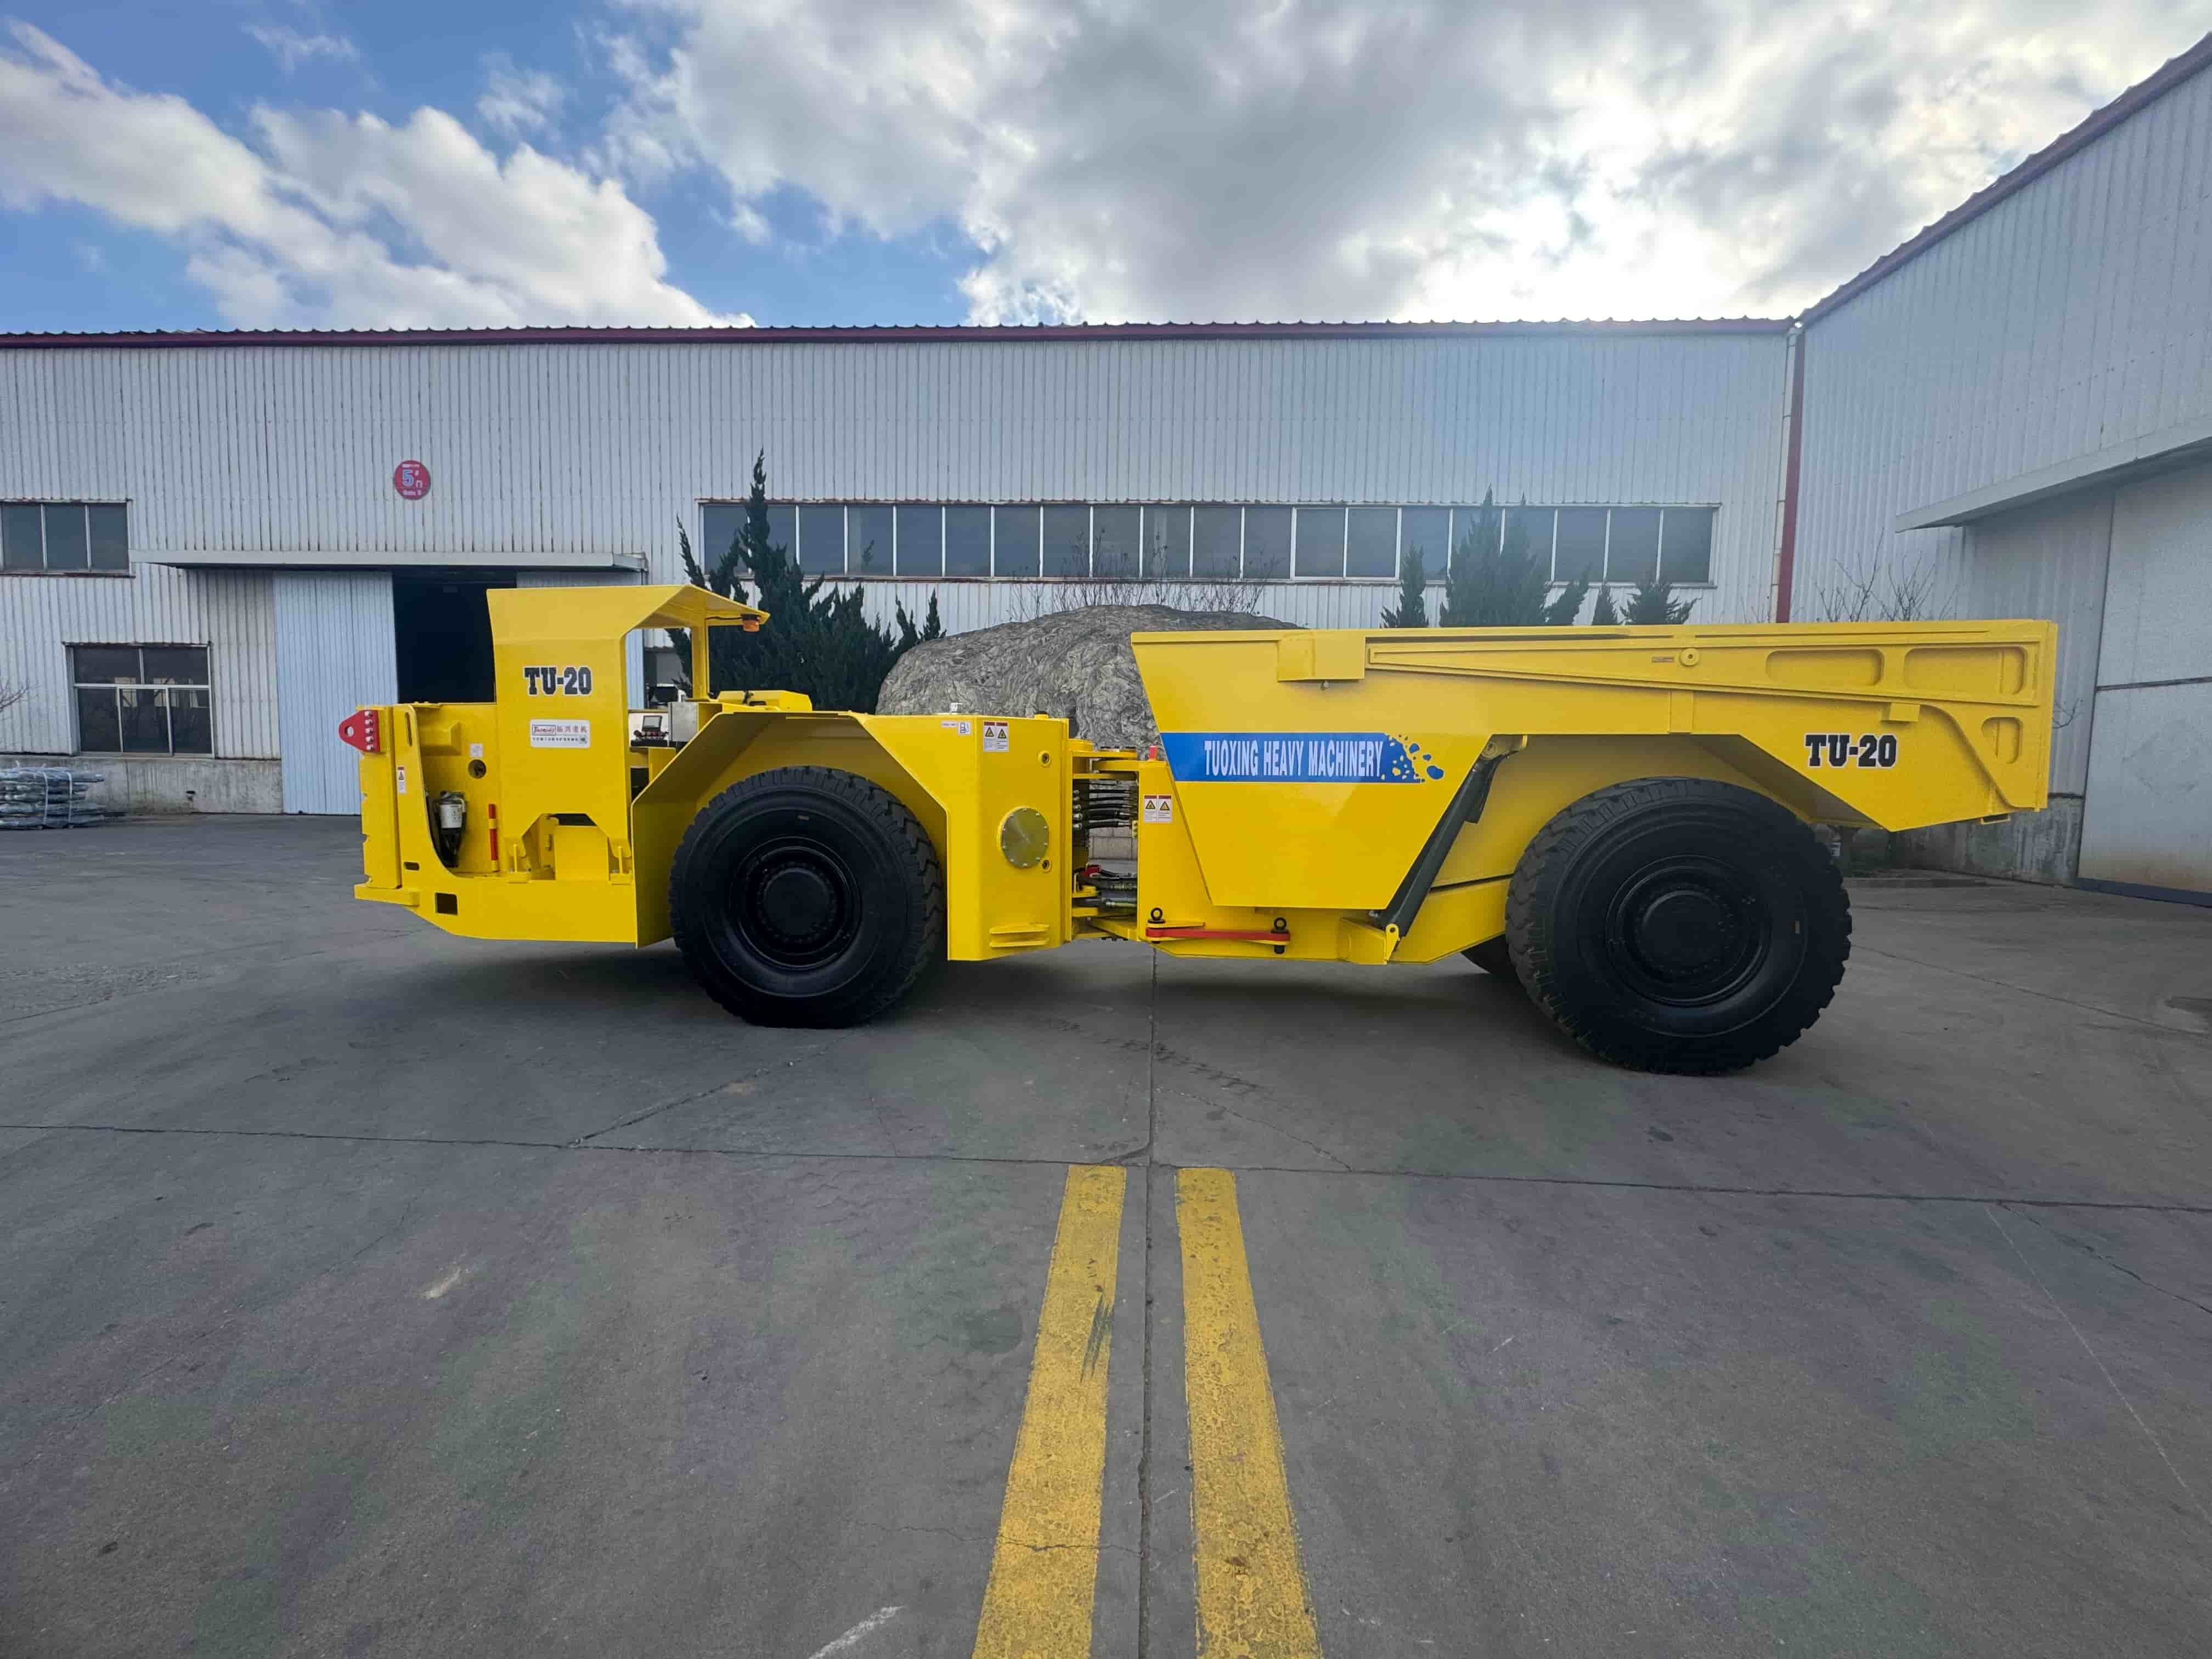
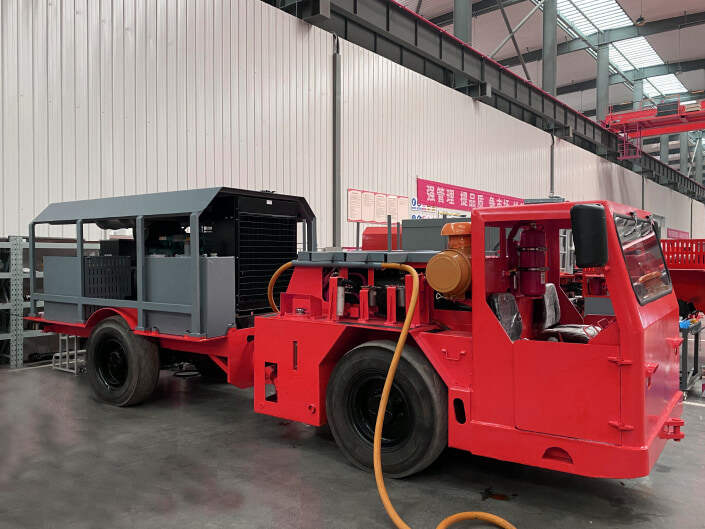
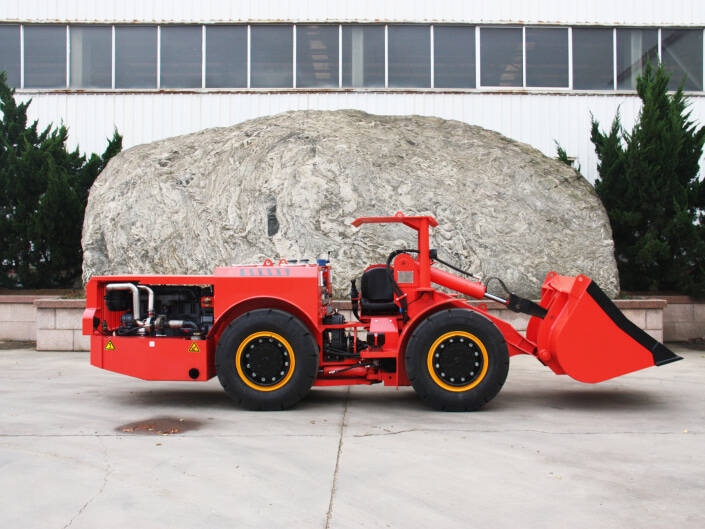
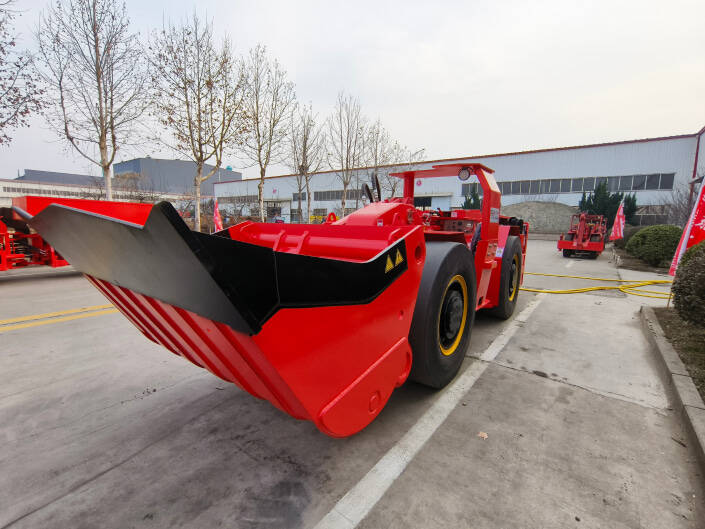
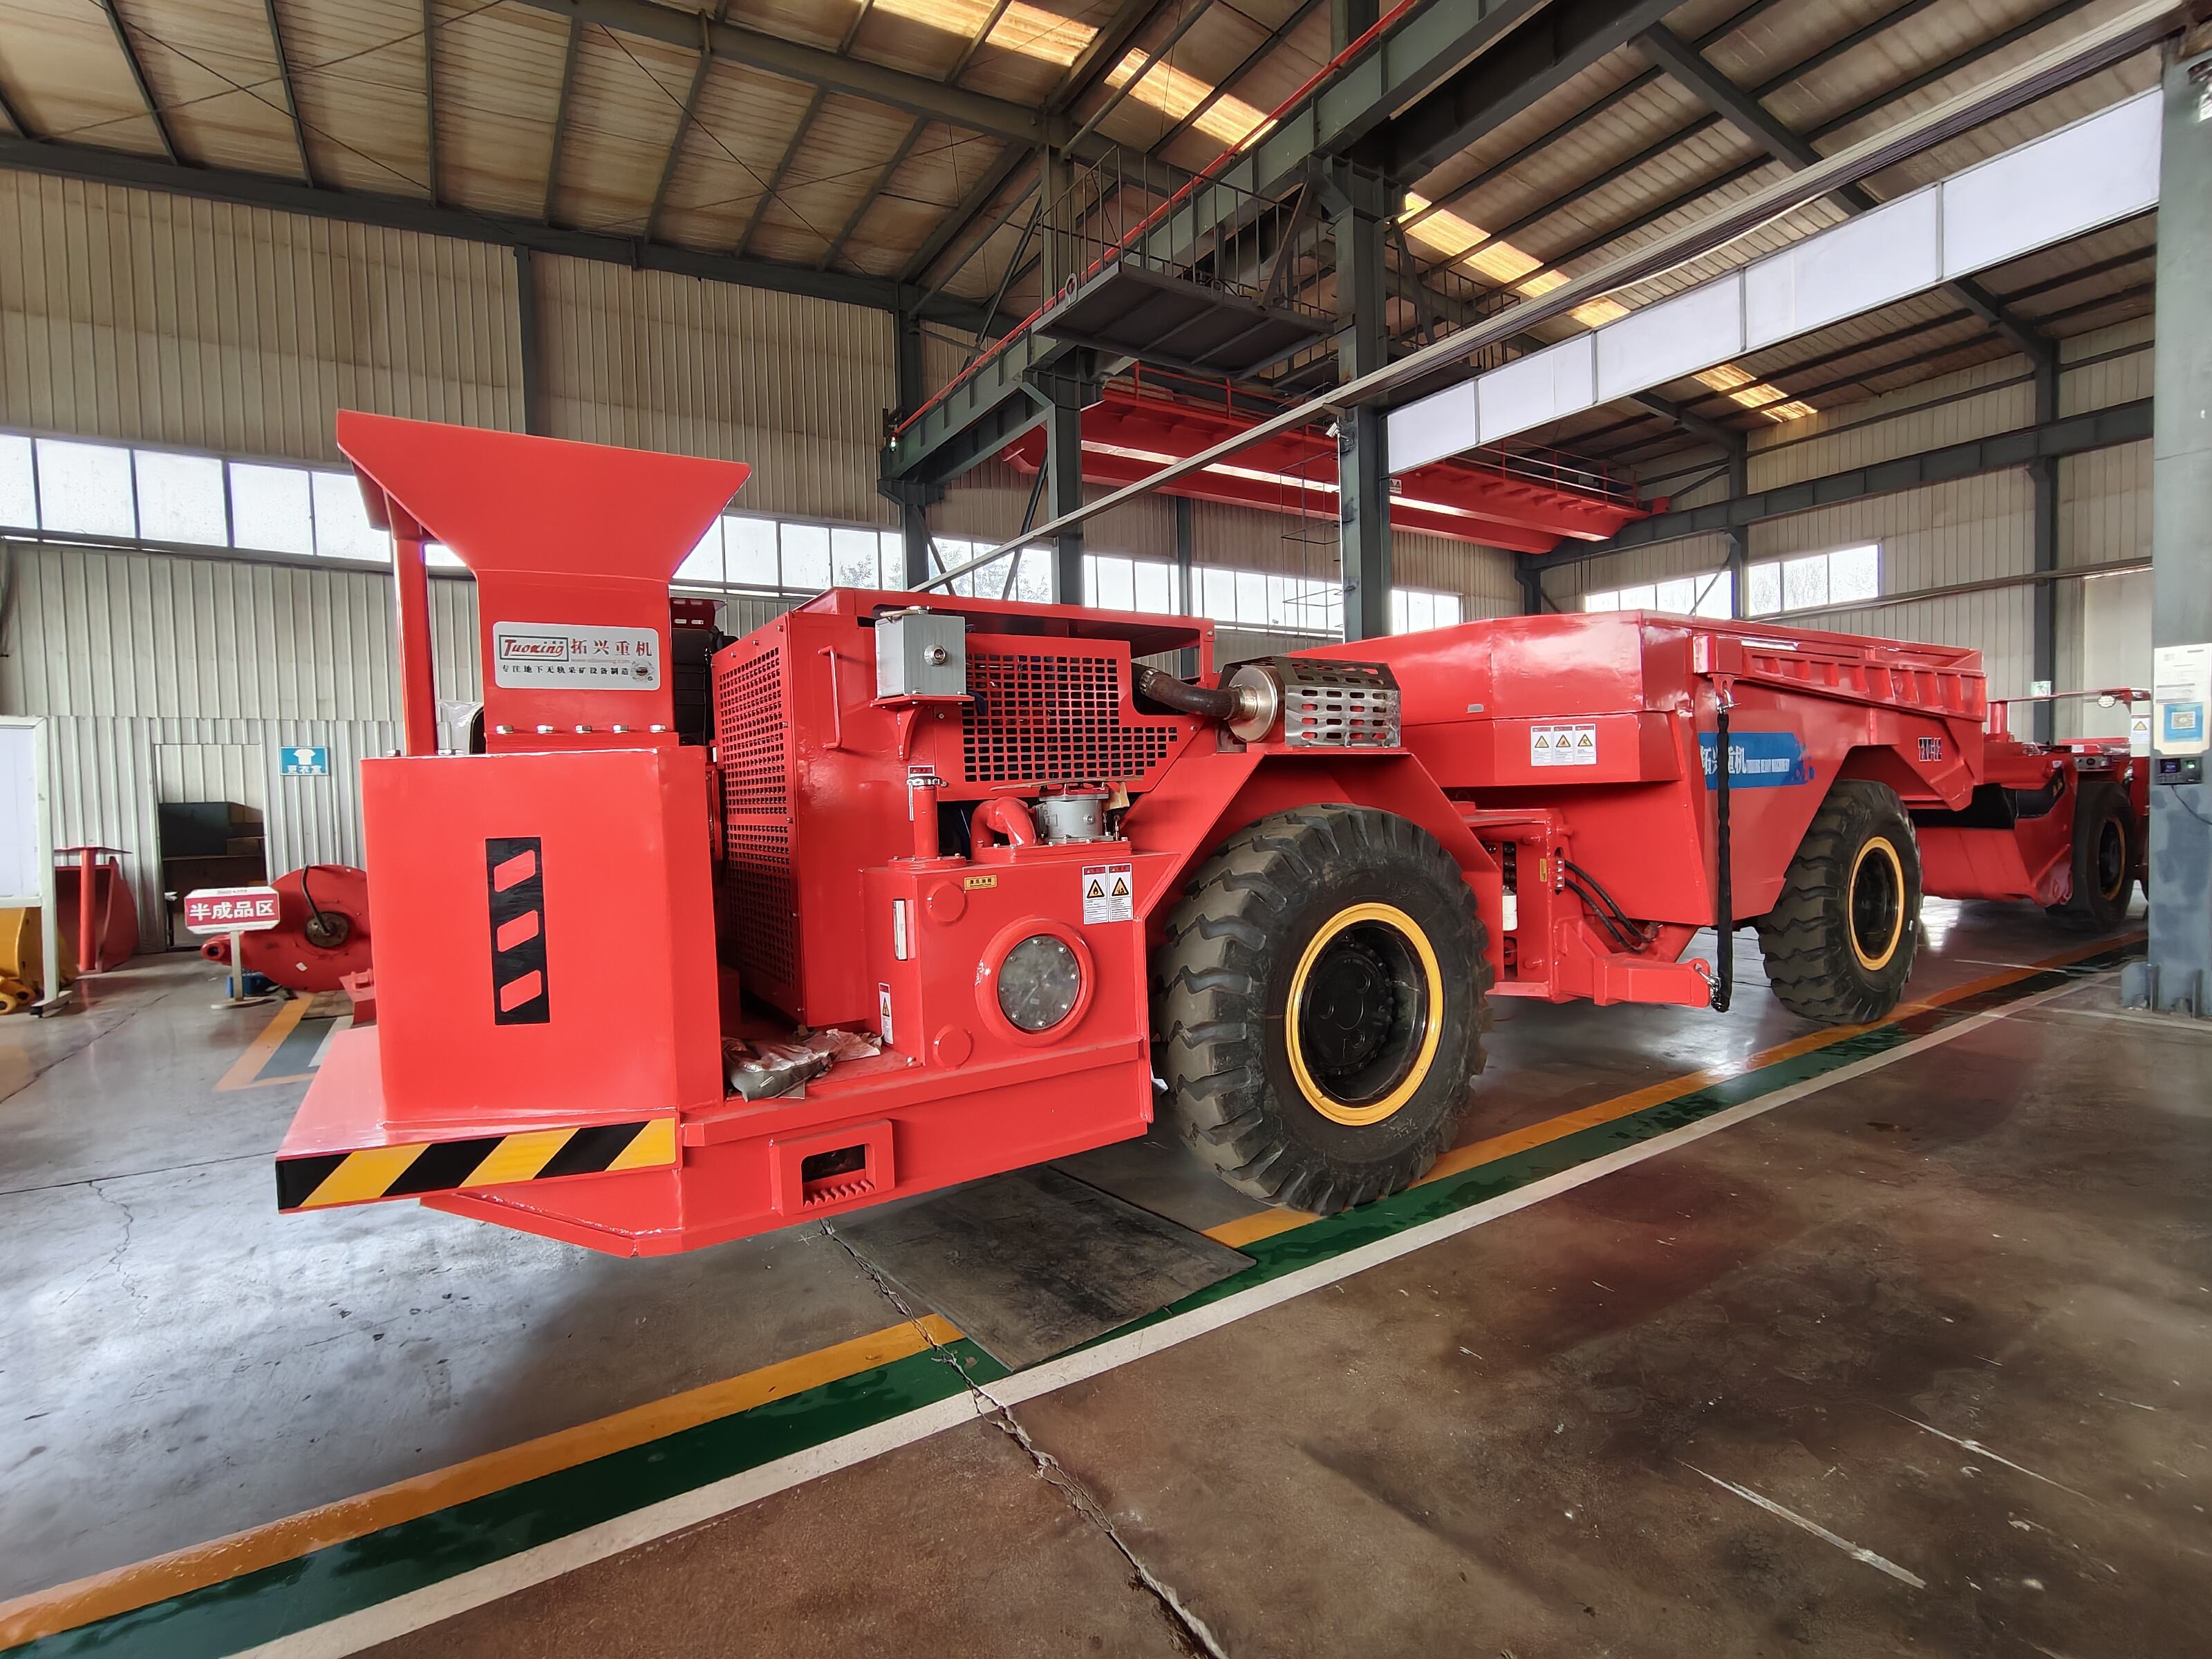
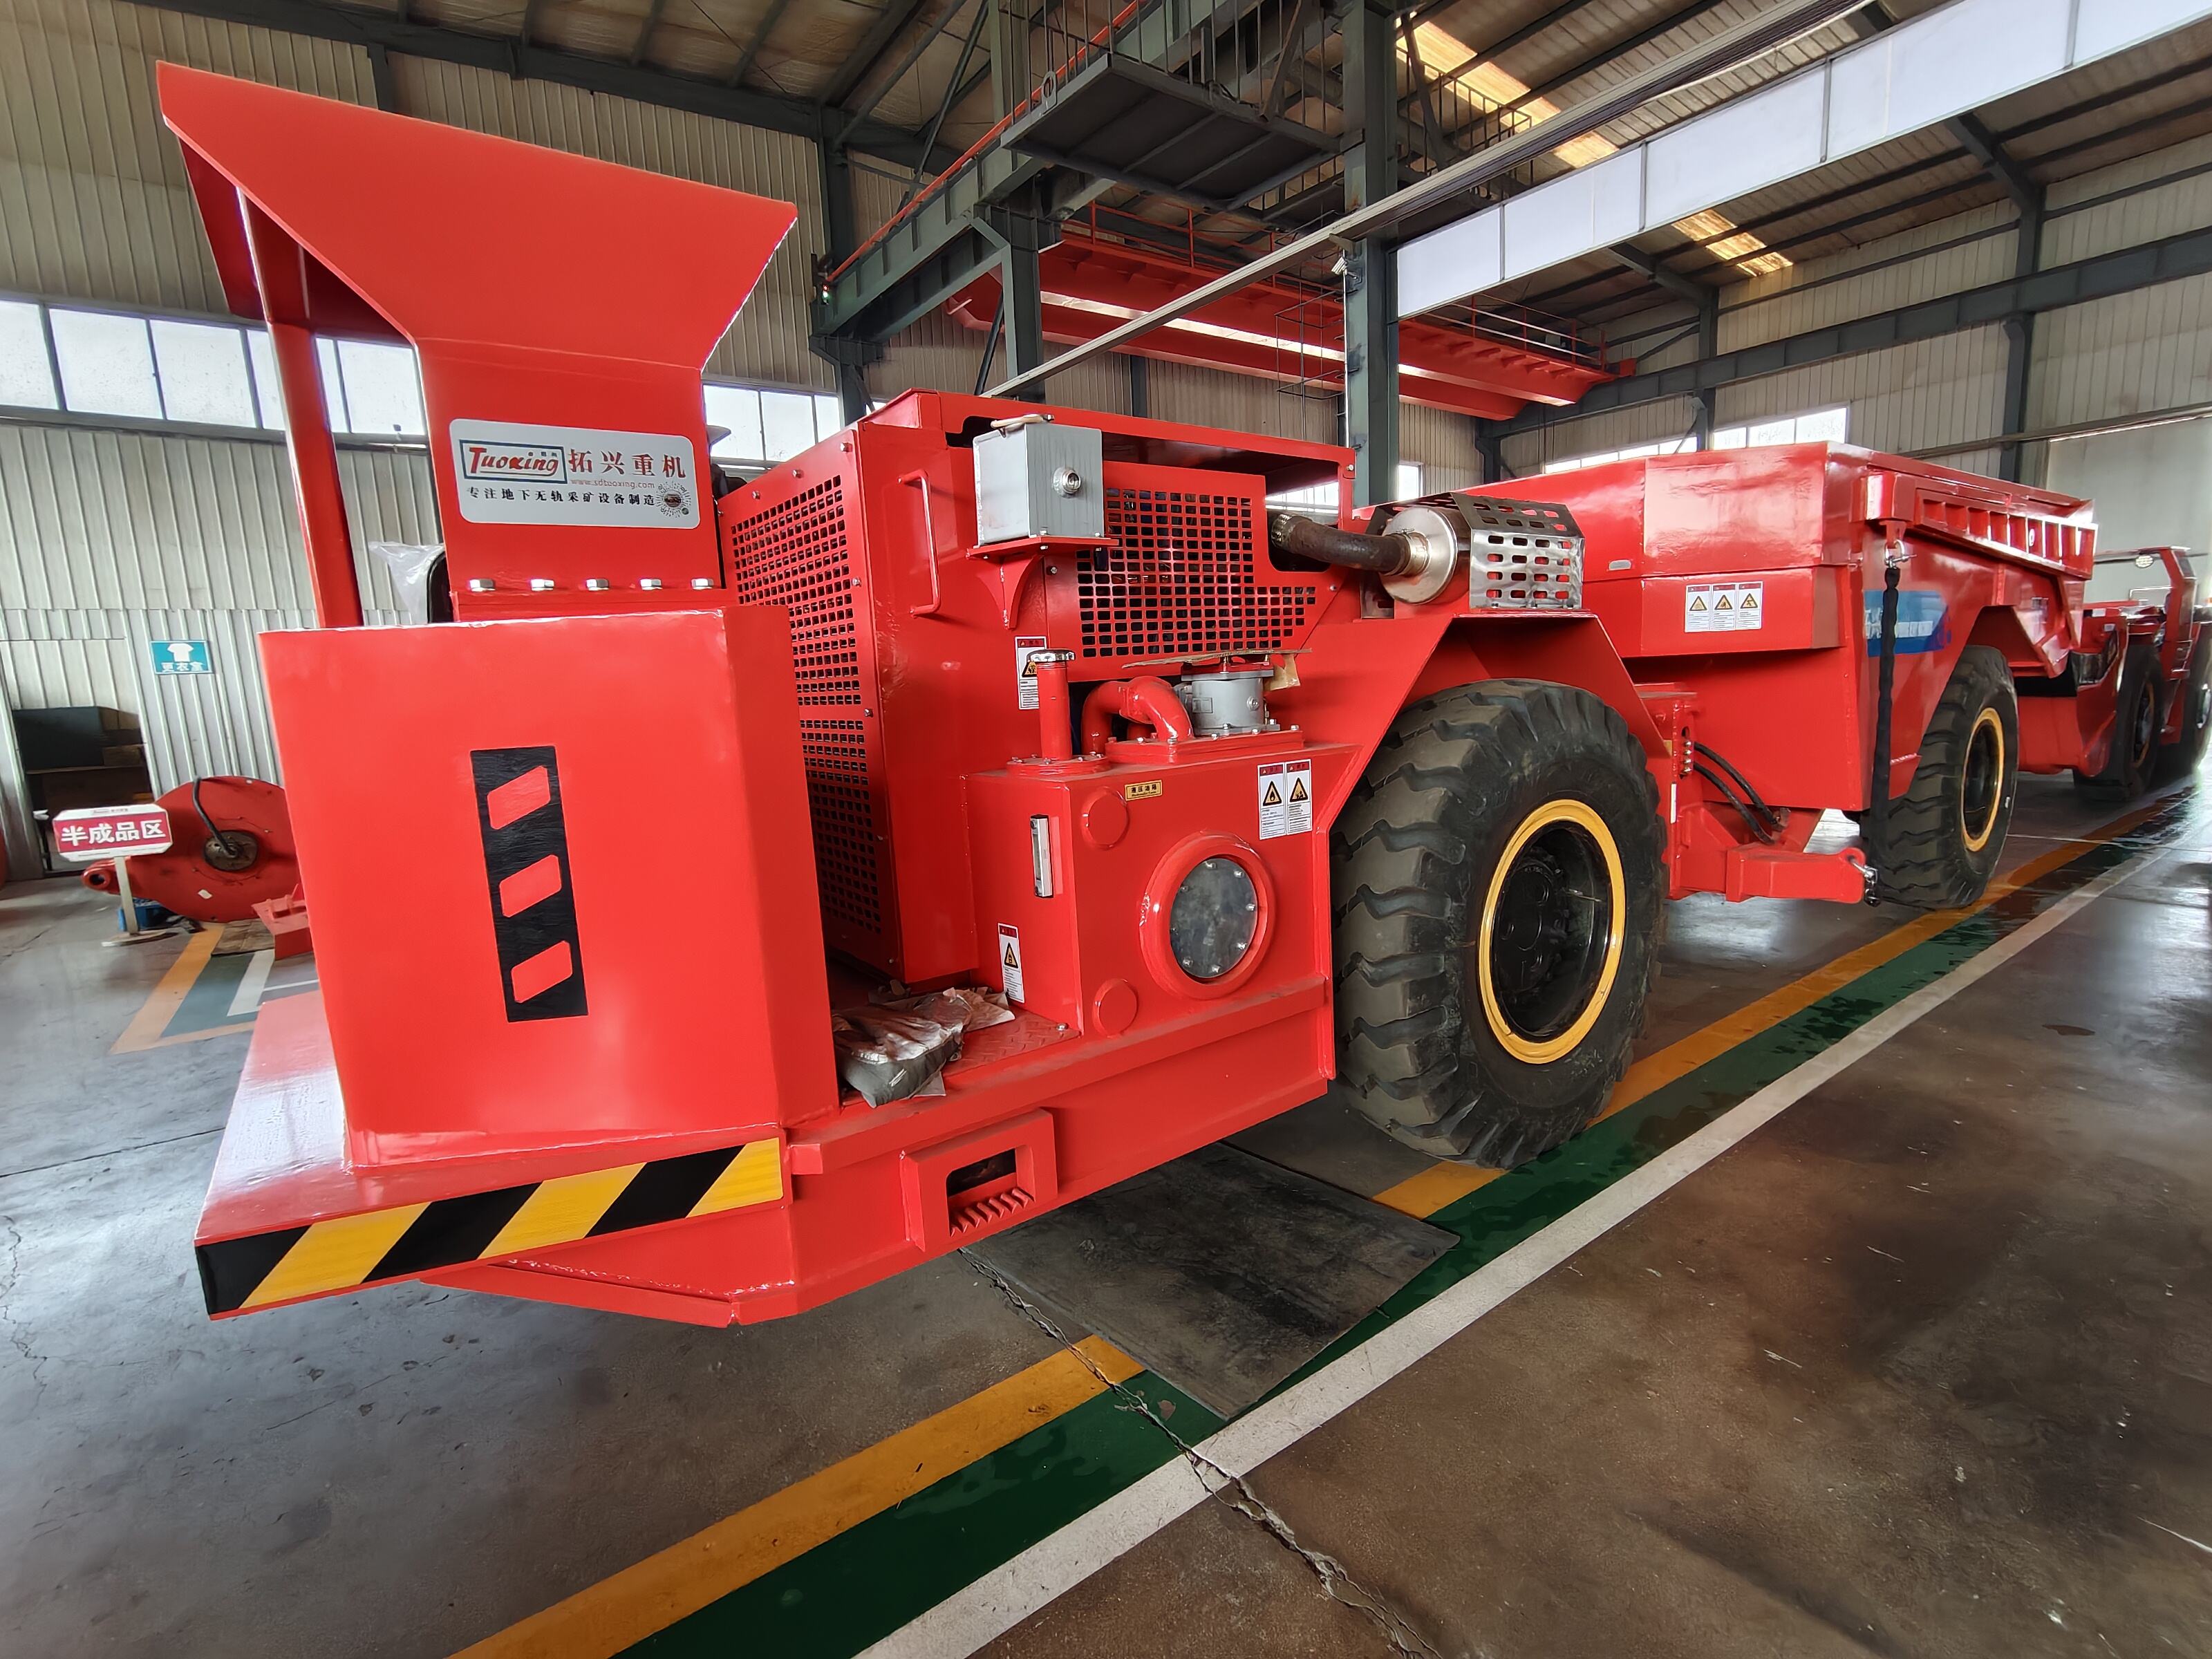
huge mining equipment
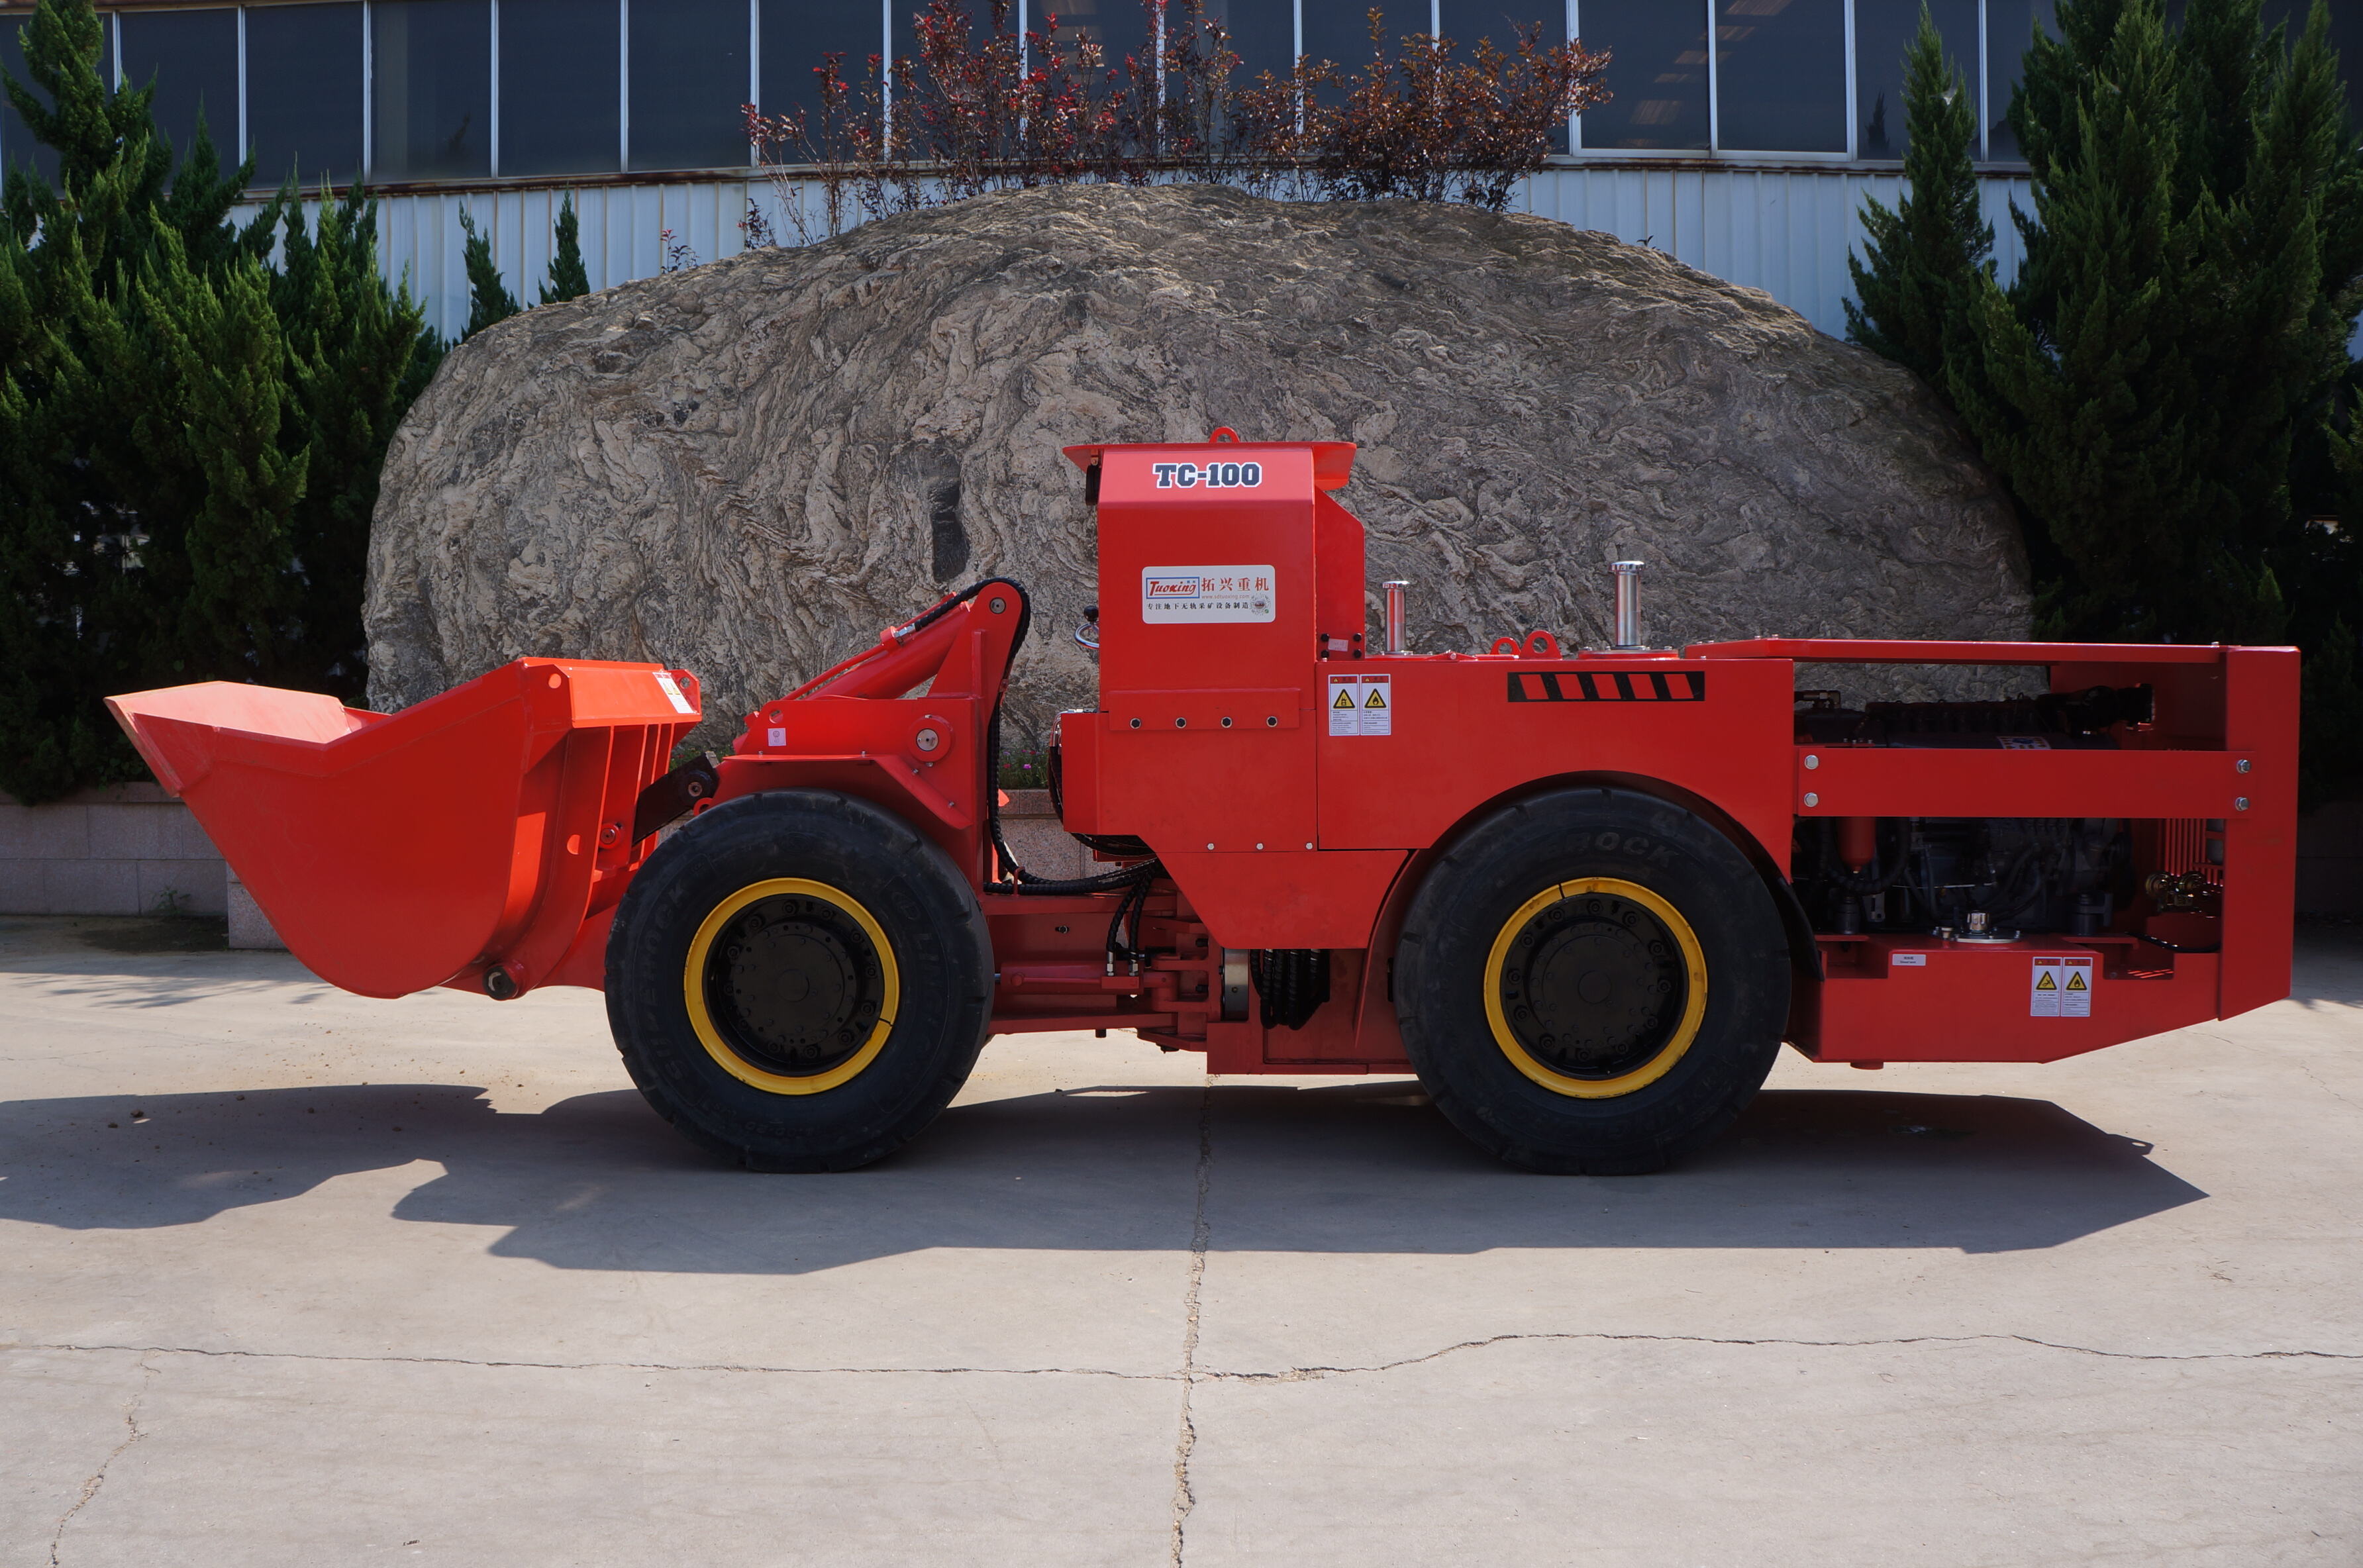
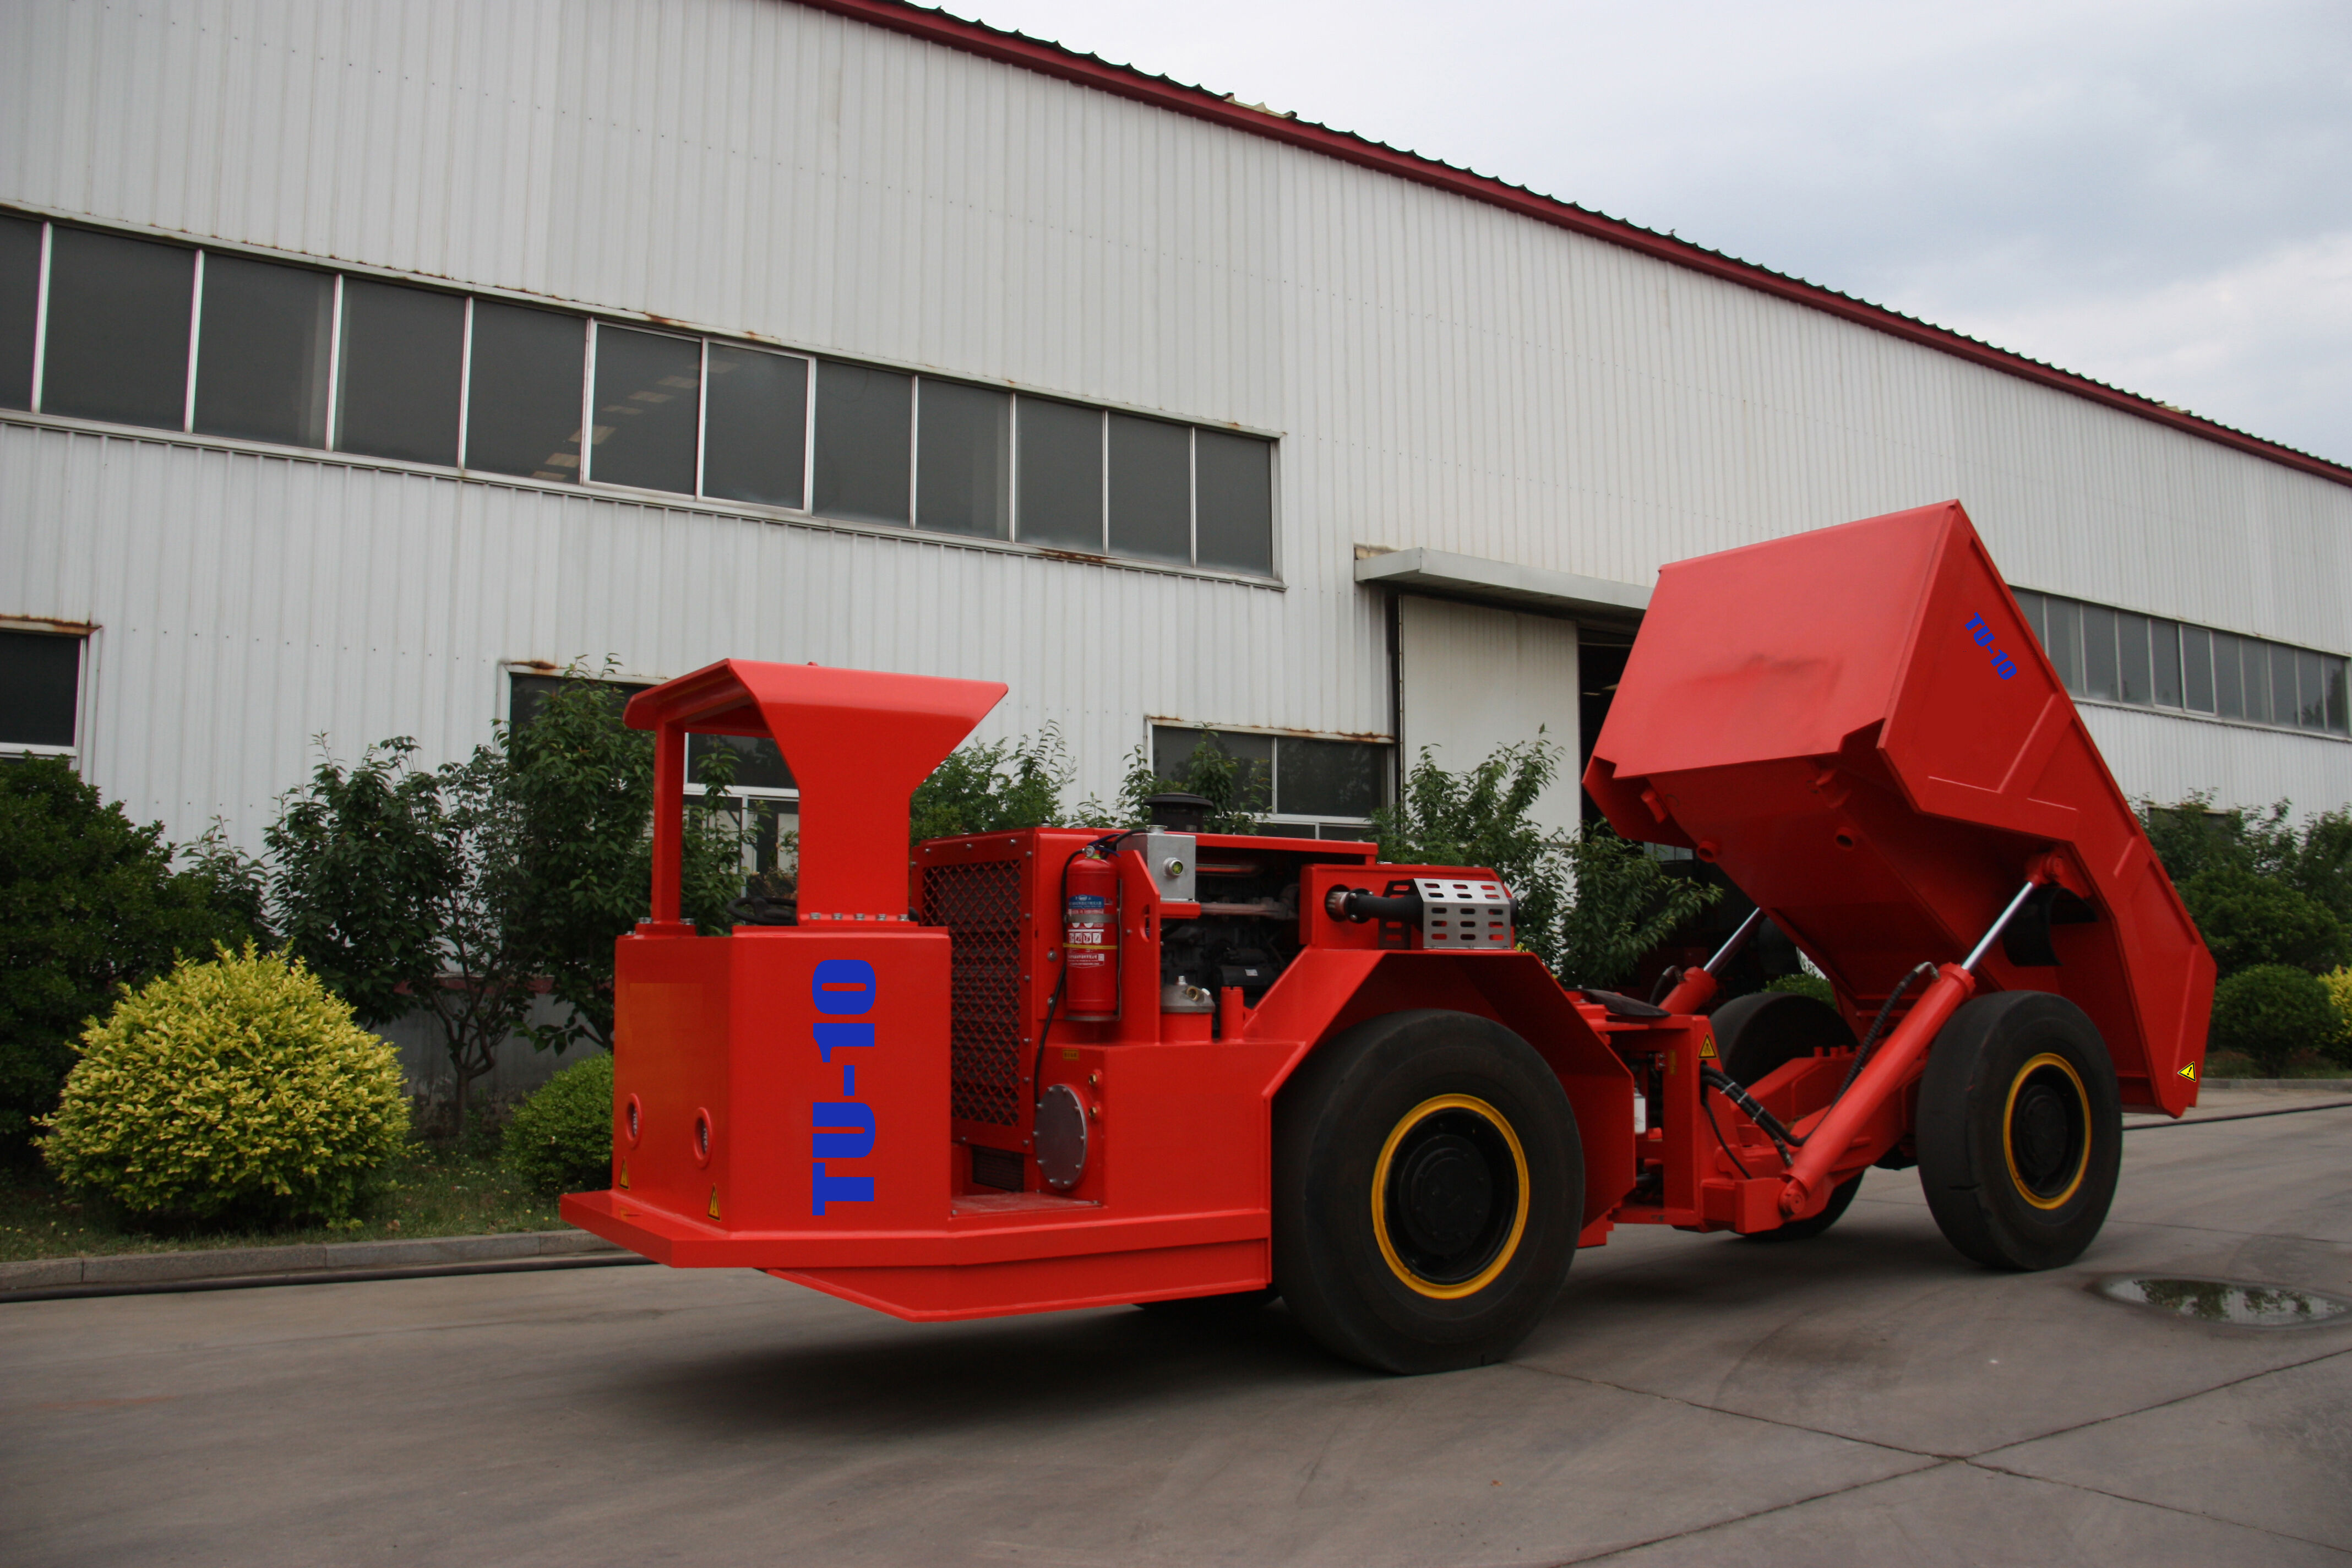
Huge mining equipment represents the pinnacle of industrial engineering, designed to extract valuable minerals and resources from the earth with unprecedented efficiency and scale. These massive machines are essential components in modern mining operations, capable of moving thousands of tons of material daily while maintaining operational excellence in the most challenging environments. The primary functions of huge mining equipment encompass excavation, hauling, crushing, and processing of raw materials from open-pit mines, underground operations, and quarries worldwide. These powerful systems integrate advanced hydraulic mechanisms, reinforced structural components, and intelligent control systems to deliver consistent performance under extreme conditions. Technological features include automated load monitoring, real-time diagnostic capabilities, fuel-efficient engine designs, and operator assistance systems that enhance safety and productivity simultaneously. The application scope of huge mining equipment extends across multiple industries, including coal extraction, metallic ore mining, diamond recovery, aggregate production, and construction material sourcing. Modern huge mining equipment incorporates GPS tracking, remote monitoring capabilities, and predictive maintenance algorithms that minimize downtime and maximize operational availability. The engineering behind these machines focuses on durability, with components designed to withstand abrasive materials, temperature fluctuations, and continuous heavy-duty cycles. Manufacturers equip huge mining equipment with spacious, climate-controlled cabins that provide operators with ergonomic workstations and comprehensive visibility of the work area. The integration of telematics systems allows mine managers to track performance metrics, fuel consumption, and maintenance schedules from centralized control rooms. As mining operations expand to more remote and challenging locations, huge mining equipment continues to evolve with enhanced mobility features, modular designs for easier transportation, and improved environmental controls that reduce emissions and noise pollution. The return on investment for huge mining equipment is realized through increased production volumes, reduced operational costs per ton, and extended equipment lifecycles that span decades with proper maintenance protocols.
 EN